Induction Coil Air Gap and Foil Distance: Centering and Height Setup
Set up an induction sealing air gap: compare measurement references, check head centering and height, and prepare a product changeover record.
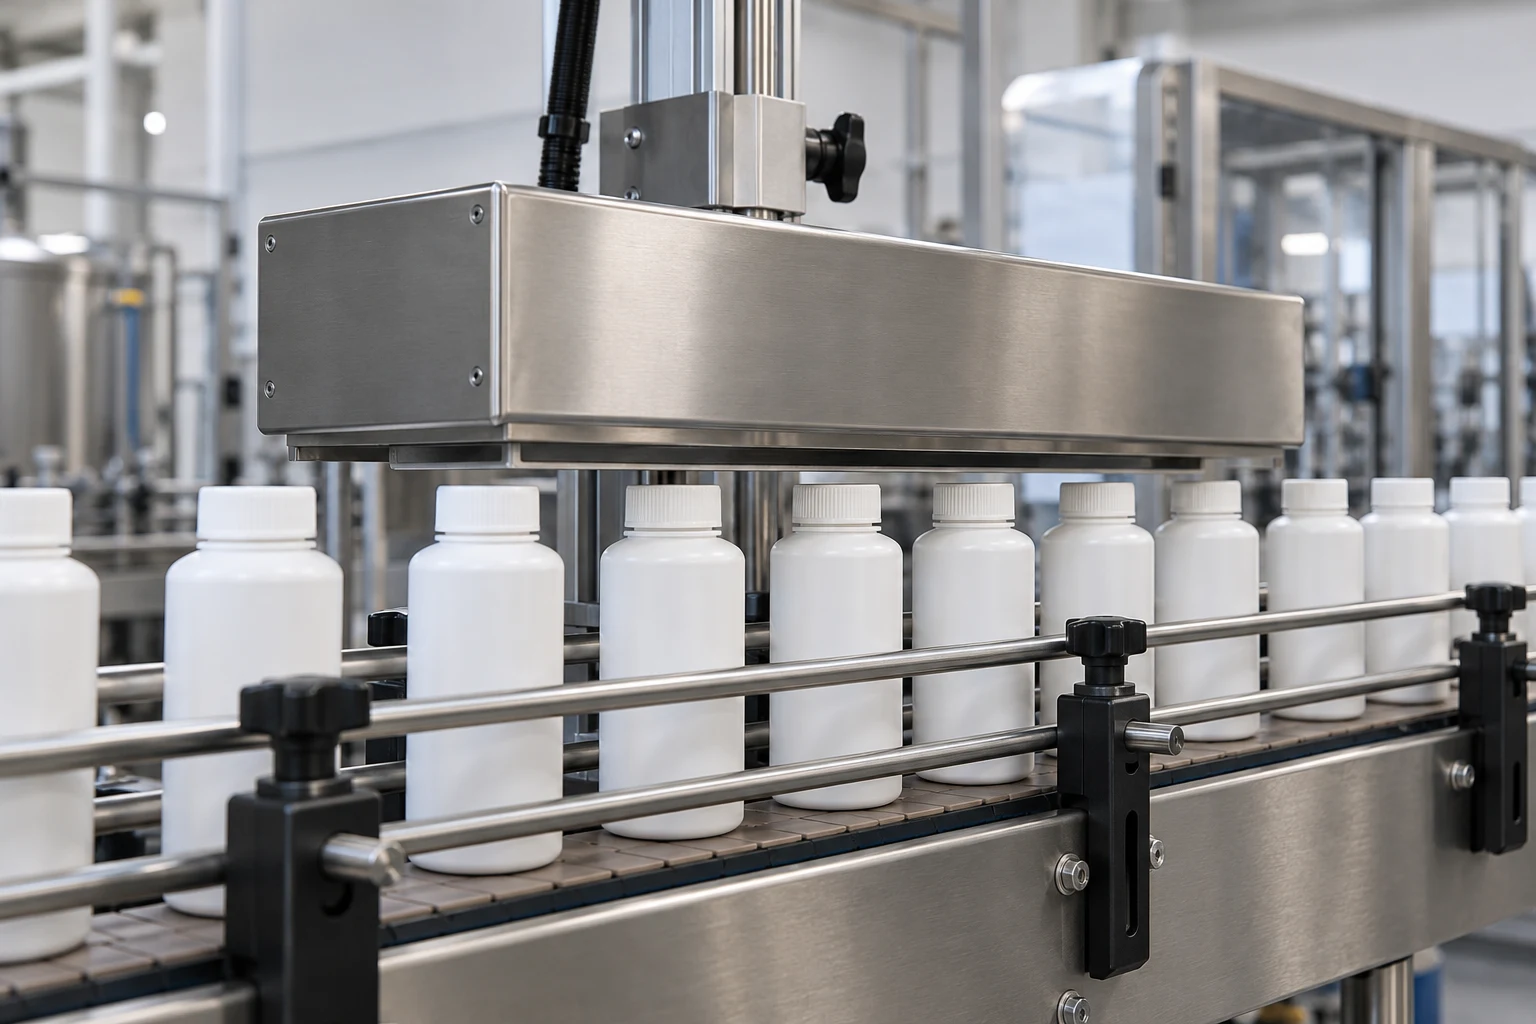
Start your induction sealing air gap setup by naming the measurement endpoints. Pillar defines the gap as the distance from the foil on the bottle to the bottom of the coil. The gap between the top of the closure and induction head must be uniform and not vary after setup.
Use the checks below to work through foil distance, induction coil height setup and the bottle path. For the wider equipment overview, see induction sealing machines.
Which gap are you measuring?
Keep the measurement reference beside the setting in your setup notes.
Sealing-head design is based on the location of the foil liner in relation to the top of the closure. As the distance between the sealing head and liner increases, the strength of the induction field it passes through decreases.
Pillar gives a rule of thumb: ensure a minimum of 3 mm clearance between the thickest cap and the sealing head. Pillar then instructs removing the cap, measuring the gap distance and standardizing that distance across cap designs.
Enercon describes the foil reference this way: ideally, the foil liner should be 1/8″ to 1/4″ away from the bottom of the sealing head. Keep that foil reference explicit when comparing it with a cap-top clearance instruction.
Center the bottle path and level the head
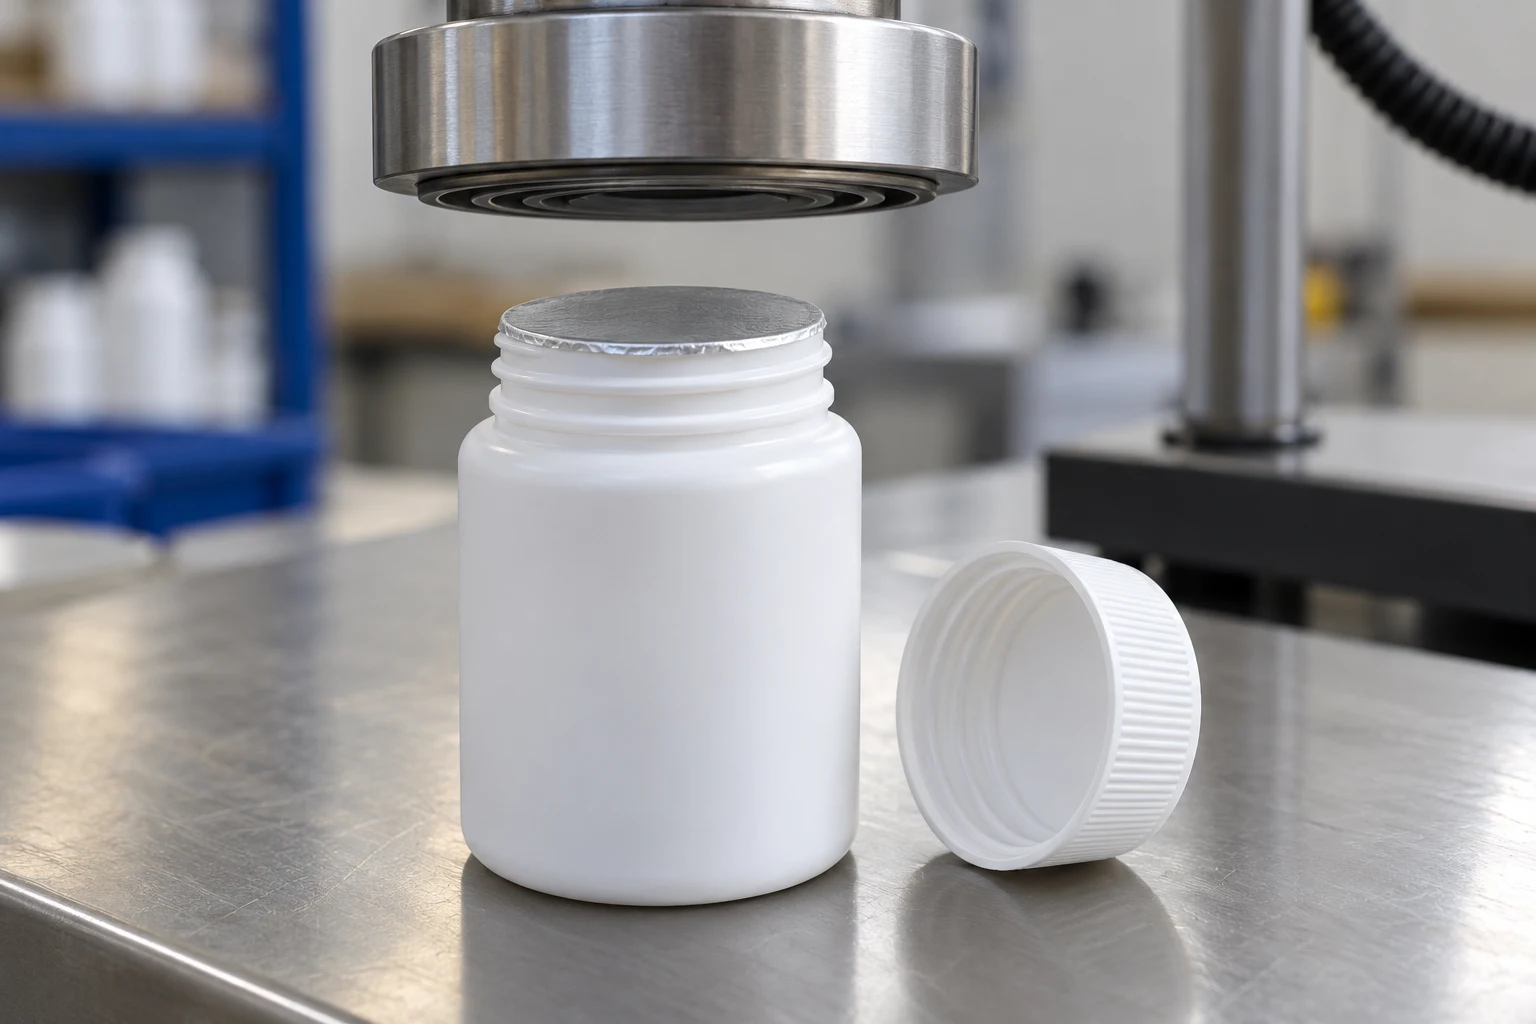
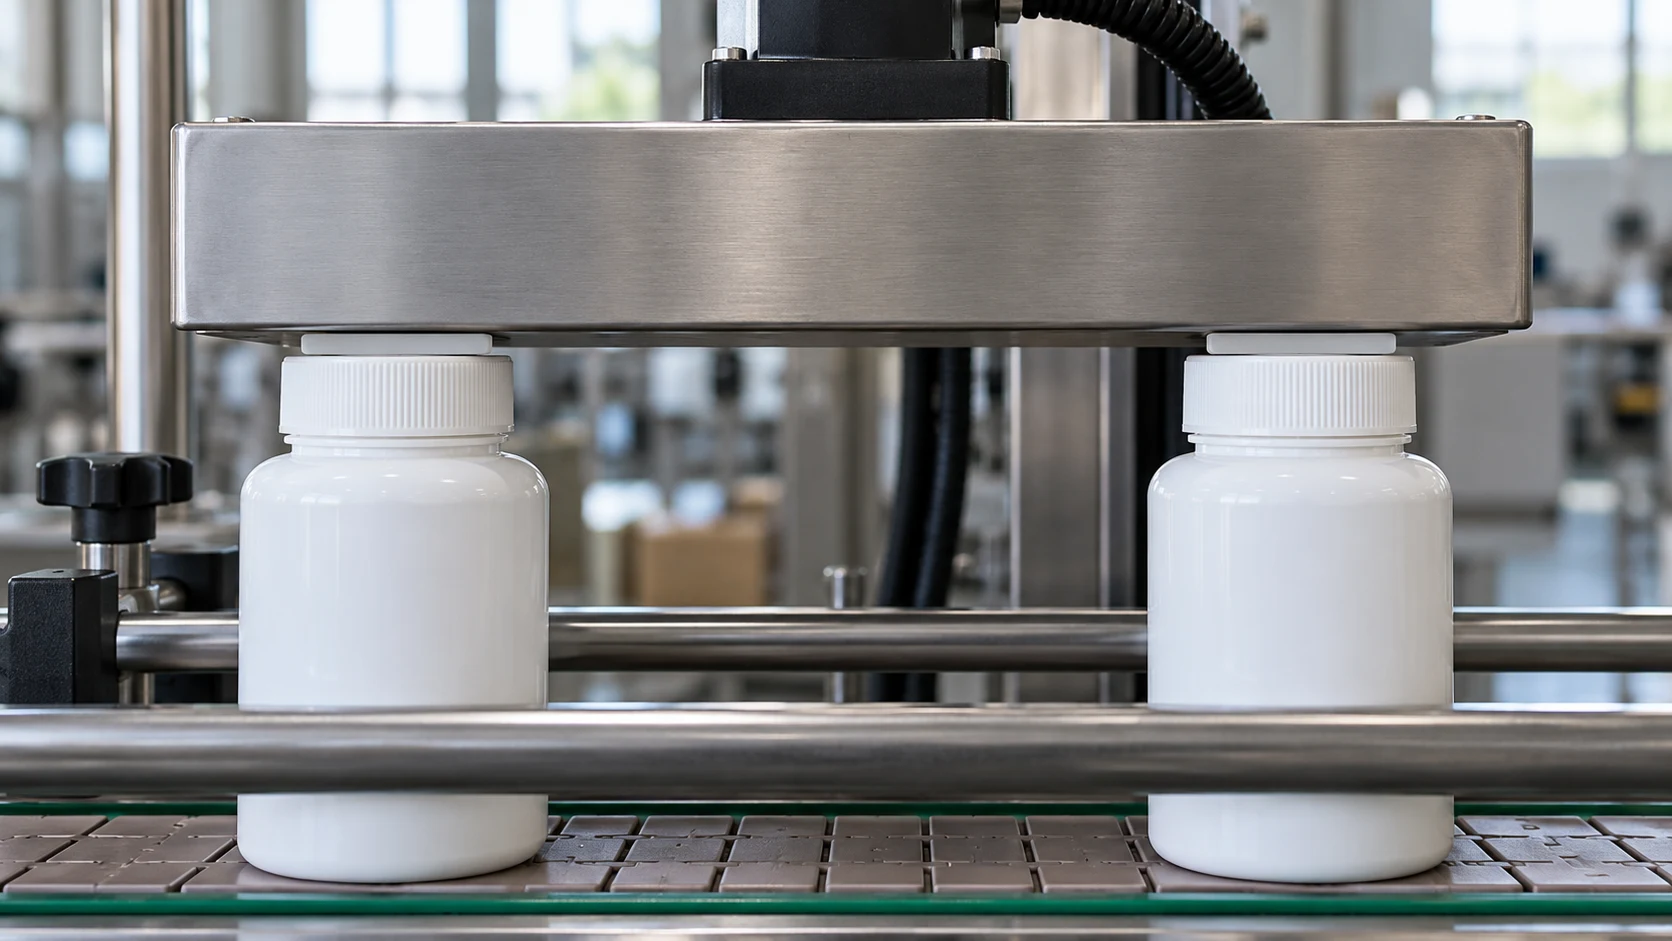
Use the alignment parameters in the sealer manual. Align the guide rails so containers enter and exit the sealing head properly centered. In Enercon’s All-In-One adjustment guide, the product must run centered along the entire length of the sealing head.
The closure must be centered in the induction tunnel. Where there is a center line, the closure center must follow it. The induction sealing head must be parallel to the top of the closure and conveyor in all directions.
Metallic guide rails near or under the sealing head can distort the induced electromagnetic field.
Check the height at the entrance and exit
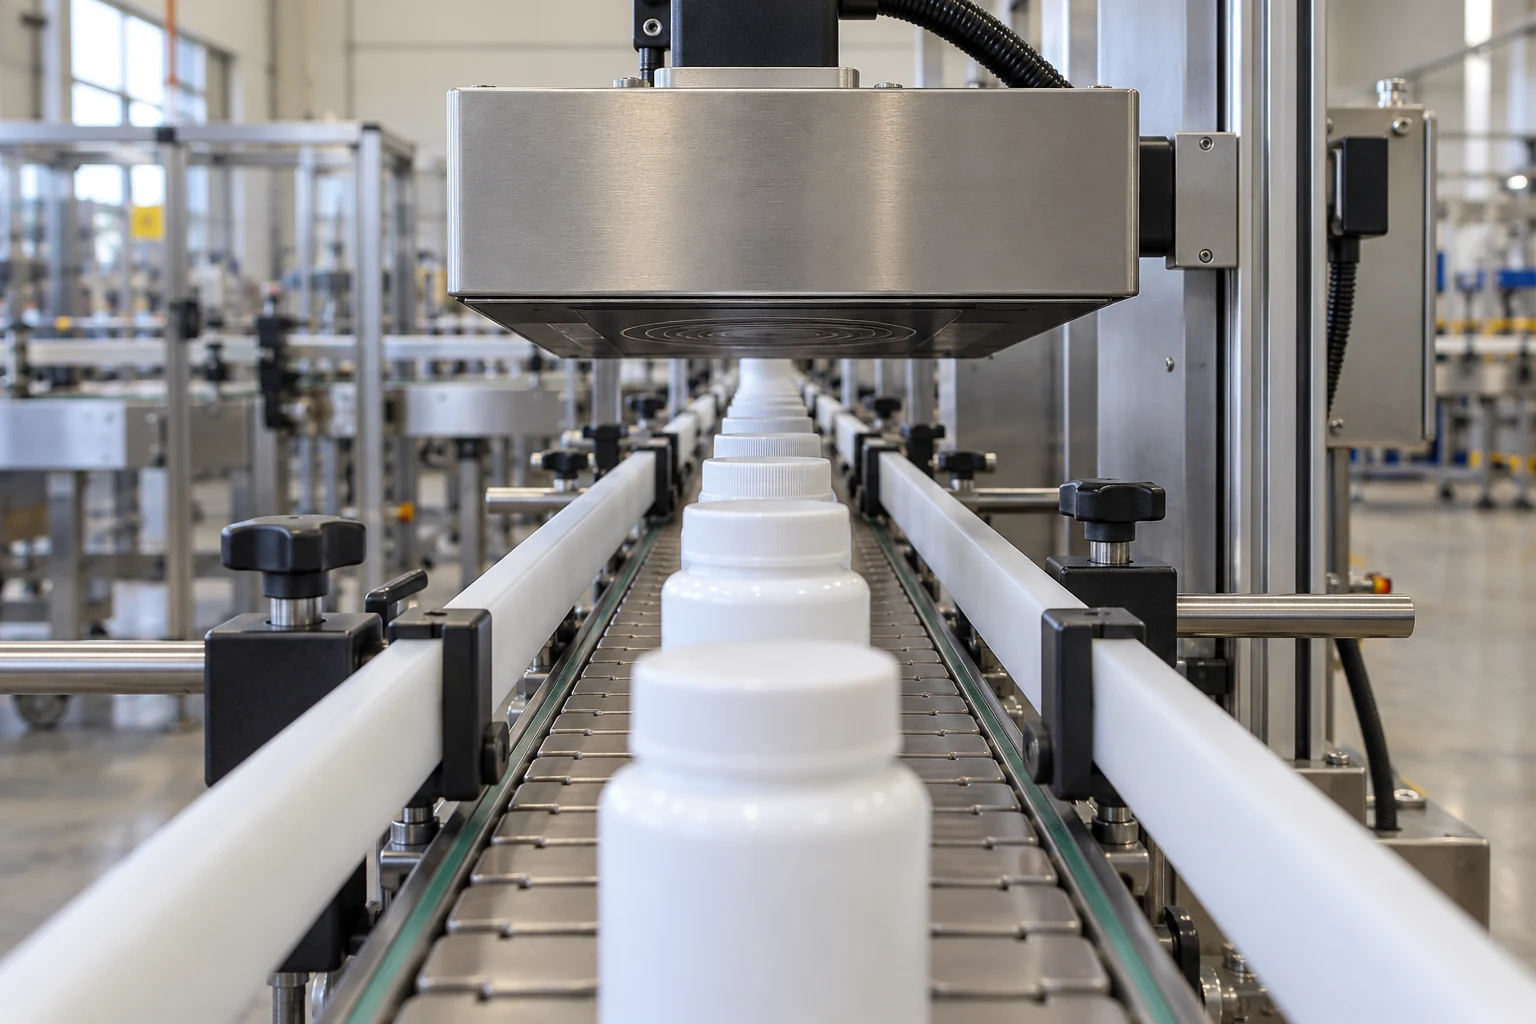
Use these checks from the Enercon Cap Sealing Handbook:
- Level and center the sealing head over the conveyor or product.
- Fill 2 containers with product to duplicate production weight.
- Place one container at each end of the sealing head.
- Place a proper-thickness gauge on top of each cap.
- The fit should be snug with no change to the gap when the gauge is removed.
Keep the height of the liner relative to the sealing head consistent.
Does a different closure change the setup?
For sports or flip top closures running in tunnel coils, the clearance depends on the internal design of the coil. For the Pillar inFinity Tunnel Coil, the indicator lines should be at the same level as the foil layer to ensure a proper seal.
For the Pillar Universal Sealing Coil, the coil should be angled to the product’s cap diameter to maximize efficiency.
For the head-selection decision, continue to flat-coil and tunnel-coil selection.
Revisit geometry when seals are weak or partial
Use these symptom checks alongside your setup record.
Weak or absent seals
Selig lists an excessively wide air space as a probable cause of weak or absent seals.
Partial seals or leakers
Selig lists head alignment that is not parallel, centered and level to the closure as a probable cause of partial seals or a high percentage of leakers.
Overheated or burnt seals
If the distance between the sealing head and the foil liner is too small, it can cause the seals to overheat or burn. Too much power can create burnt liners.
Continue with the broader induction sealing troubleshooting guide for the next part of your investigation.
Secure the setup and keep a changeover record
Securely fasten the induction equipment to the floor so that the sealing head cannot be bumped or vibrate out of alignment. When checking on-torque and seal integrity, you should also check the induction head alignment. Keep a record of the setup information for each product run. This information helps ensure consistent and accurate changeover between products.
Use the following blank prompts for your next setup record:
- Package, cap and liner identification: ______
- Coil model and orientation: ______
- Cap-top clearance reference and reading: ______
- Foil-to-coil reference and reading: ______
- Cap-top thickness or closure drawing reference: ______
- Entrance and exit gauge checks: ______
- Guide-rail positions and observed cap path: ______
- Conveyor speed and power setting: ______
- Seal-integrity observations: ______
- Operator and date: ______
Keep this record with your next changeover discussion. Continue to seal integrity testing for the verification topic.
Sources
- Pillar Technologies — Ways to Improve Your Induction Sealing Results
- Pillar Technologies — Additional Sealing Coils
- Selig Group — PHT Book
- Selig Group — FAQs & Troubleshooting
- Enercon — Cap Sealing Handbook
- Enercon — All-In-One Sealing Head Adjustment Guide
- Enercon — Optimizing an Induction Field for Cap Sealing
- Enercon — Improve Your Induction Cap Sealing IQ
- Enercon Industries Limited — Adaptive Sealing Gap
More about Induction Sealing Machines
Electromagnetic induction cap sealers, flat vs. tunnel sealing coils, kW power-to-line-speed matching, capping head integration, and troubleshooting.
Related Articles
Hot-Fill vs Cold-Fill Induction Sealing: Foil Heating Window and Headspace Pressure
Compare hot-fill and cold-fill induction sealing, then qualify the heating window, neck fit and cooled-pack integrity before transferring a line recipe.
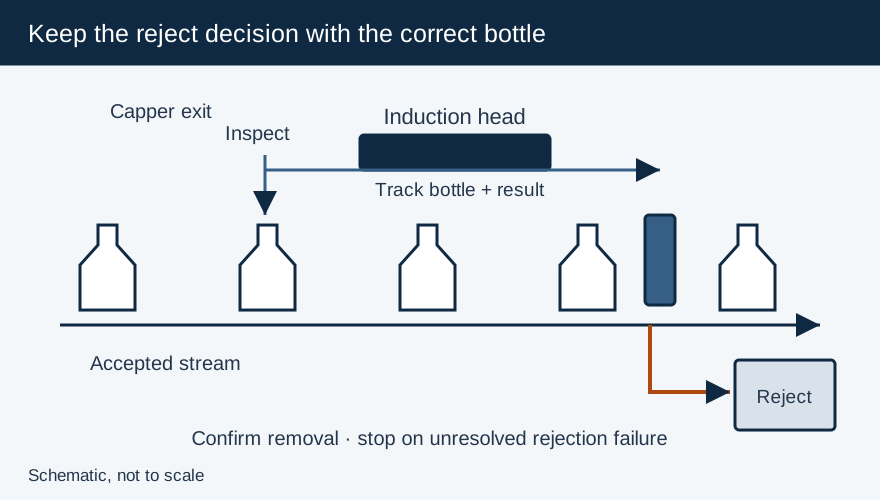
Capping and Induction Sealing: Line Interfaces and Rejection
Specify capper-to-sealer transfer, conveyor stop protection, inspection signals and confirmed rejection for an induction sealing line.
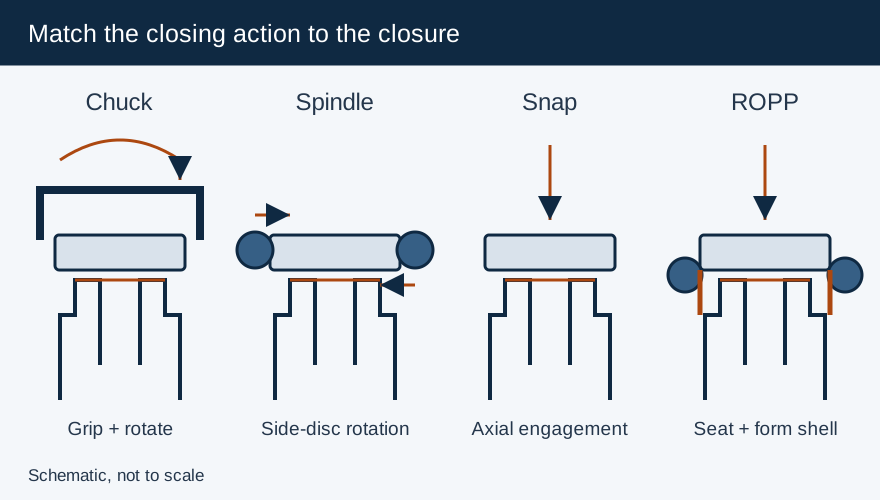
Capping Machines Explained: Match the Cap, Container and Closing Process
Compare chuck, spindle, snap and ROPP closing mechanisms, then specify container support, torque checks and the capper-to-sealer interface.